Non-Magnetic HWDP for Drilling | API Spec 7-1
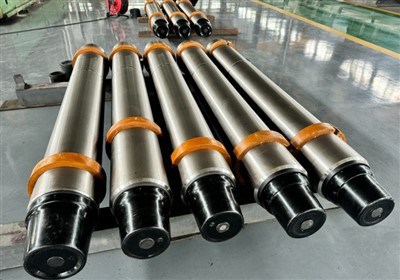
Non-magnetic HWDP is used in the transition zone between standard drill pipes and drill collars to reduce fatigue failures and absorb bending stresses. Our HWDP is made from high-strength and low-carbon austenitic stainless steel or copper-free alloy bars, extending the magnetic-free zone above the BHA for better MWD performance. Available with or without hardbanding, these pipes feature thick walls and special wear-resistant features, fully compliant with API 7-1 standards for demanding directional drilling operations.
-
![Non-Magnetic Heavy Weight Drill Pipe]() Non-Magnetic Heavy Weight Drill PipeNon-magnetic heavy weight drill pipes (HWDP) are essential components within directional drilling, MWD/LWD, and medium-deep well assemblies, positioned between drill pipes and collars. They fulfill
-
![Non-Magnetic Pressure-Bearing Drill Pipe]() Non-Magnetic Pressure-Bearing Drill PipeNon-magnetic pressure-bearing drill pipe Drill pipes are an essential component of the high-pressure drilling system of directional drilling, MWD/LWD (mud testing while drill, logging while drilling)
-
![Non-Magnetic Stabilizers for Coal]() Non-Magnetic Stabilizers for CoalAs a downhole tool for coal mine directional drilling, gas storage, and CBM production, non-magnetic stabilizers for coal are designed for coal mines' operating conditions (narrow road,
-
![Non-Magnetic Joints for Coal]() Non-Magnetic Joints for CoalWithin the coal mine drill string, a non-magnetic connection zone is implemented. This zone removes magnetic field interference for specialized downhole instruments, including gas concentration
-
![Coal Machine Non-Magnetic Drill Pipe]() Coal Machine Non-Magnetic Drill PipeCreate a continuous non-Magnetic channel on coal machine drill string (dispose of magnetic field on coal mine-specific precision tools (gas concentration sensor, borehole trajectory detector, coal


Product Types
Non-Magnetic Drill Collars (NMDC):
Solid bored tubular bars providing a non-magnetic housing window for directional survey sensors.
Non-Magnetic Stabilizers:
Integral-blade and welded-blade units maintaining wellbore trajectory while preserving magnetic isolation.
Non-Magnetic Heavy Weight Drill Pipe (HWDP):
Non-Magnetic Heavy Weight Drill Pipe (HWDP): Transitional drill string members offering mechanical flexibility and weight-on-bit control.
Non-Magnetic Crossover Subs (X-Over):
Connection adapters linking different API thread configurations without magnetic signal interference.
Applications
Underground Gas Drainage Boreholes:
Guiding long-distance horizontal boreholes along coal seams to relieve methane pressure ahead of extraction.
Directional Exploration Drilling:
Mapping geological anomalies, fault lines, and seam boundaries prior to face operations.

MWD and LWD Tool Housing:
Protecting electronic survey packages from high shock, vibration, and magnetic field distortion.
Geothermal and Trenchless Boring:
Providing non-magnetic sensor housings for precision utility and shallow directional installations.
Material and Technical Specifications
|
Property |
Specification |
|
Material Grades |
Premium Low-Carbon Austenitic Stainless Steel (P550 equivalent); Copper-Beryllium (CuBe) for specialized low-magnetic requirements |
|
Relative Magnetic Permeability |
Maximum 1.010, certified according to MIL-STD-281 and ASTM A342 |
|
Yield Strength |
Minimum 100–140 ksi (689–965 MPa), depending on outer diameter |
|
Tensile Strength |
Minimum 110–150 ksi (758–1034 MPa) |
|
Hardness Range |
284–341 HBW (Brinell Hardness) |
|
Available Outer Diameter (OD) |
73–203 mm (2-7/8–8.0 inch), sized for underground coal drilling rigs |
Manufacturing and Processing
Forging and Radial Hot Rolling: Raw alloy ingots undergo heavy rotary forging to refine crystal grain structure and eliminate internal micro-porosity.
Cold Working: Controlled cold-working processes impart uniform mechanical strength and deep surface hardness across the bar profile.
Deep-Hole Gun Drilling: Precision boring utilizing multi-axis CNC gun-drill systems to maintain concentricity and wall thickness tolerances within 0.5 mm over full bar lengths.
Thread Machining: Rotary shoulder threads cut on CNC lathes using single-point carbide inserts, paired with thread gauging and optical profile verification.
Quality Inspection
Magnetic Permeability Testing:
100% testing of every raw bar and finished component via a Förster fluxgate magnetometer to confirm permeability under 1.010 along the entire length and end faces.
Non-Destructive Testing (NDT):
Full-length ultrasonic examination for internal flaws and wet fluorescent magnetic particle inspection on all finished thread roots.
Mechanical Property Tests:
Tensile testing, Charpy V-notch impact testing, and Brinell hardness testing performed on test coupons removed from production lots.
Dimensional and Thread Metrology:
3-axis CMM and API certified thread ring and plug gauges verifying pitch diameter, lead, taper, and standoff.
How to Choose the Right Coal Drilling Tool
Match Rig Specifications: Verify spindle torque, pullback capacity, and mast clearance limitations of your underground drilling equipment to determine acceptable outer diameters and lengths.
Verify MWD Sensor Requirements: Review the magnetic clearance length specifications of your directional survey tools to select the proper non-magnetic collar length.
Select Connection Types: Specify standard API rotary connections matching your existing drill string inventory to eliminate unnecessary crossover adapters.
Evaluate Formation Abrasiveness: Choose tungsten carbide chip hardbanding on stabilizer blades when drilling through abrasive sandstone and quartz-bearing coal measures.
OEM and ODM Engineering:
Custom outer diameters, inner diameters, and overall tool lengths matched to specific underground coal rig layouts.
Specialized Connections:
Non-standard metric threads, proprietary high-torque connections, and lifting recess designs machined directly from technical drawings.
Surface Treatments:
Manganese phosphate coating, zinc-nickel plating, or heavy-duty anti-corrosion compound application for extended storage protection in humid underground environments.
FAQ
As one of the most professional non-magnetic hwdp manufacturers and suppliers in China, we also support customized service. With abundant experience, we warmly welcome you to buy high quality non-magnetic hwdp for sale here from our factory. Contact us for more details.